Top Filling Machine Selection: What to Look For in Modern Equipment
2026-10-17
Filling machines all look impressive in a brochure. But once they hit your floor, the real questions surface: Will it handle your product without foaming? Can it switch formats without an engineer on standby? Will the promised speed survive a full shift? If you skip these questions, you’re not buying efficiency—you’re buying downtime. At Wanying Machinery, we’ve learned that the best selection process starts with your filler’s daily reality, not its spec sheet. Here’s what modern equipment should deliver before you sign off.
Precision That Pays for Itself
Small deviations in measurement have a way of compounding into expensive rework, wasted material, and missed deadlines. When every cut, alignment, and tolerance is held to a tighter standard, the result isn’t just a nicer finish — it’s a direct reduction in the hours spent fixing what should have been right the first time. Precision becomes less about bragging rights and more about keeping the margin where it belongs.
That kind of reliability compounds across a production run. Tools and processes that hold their calibration longer mean fewer interruptions for adjustment, fewer rejected parts at inspection, and a steadier flow from raw stock to finished product. The upfront cost of better accuracy fades quickly when the alternative is constant correction.
Automation Without the Complexity
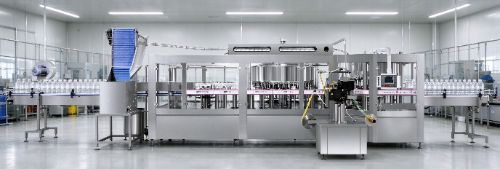
Most automation platforms expect you to learn a new language, map out endless flows, or hire a specialist just to send a follow-up email. That approach quietly drains time instead of giving it back. This tool strips away the nonessential layers and leaves only what actually moves work forward.
You choose a trigger, pick an action, and let it run. No branching trees that look like wiring diagrams, no hidden settings buried three menus deep. If something can be automated in two steps, it happens without dragging you through a setup ritual.
The real difference shows up weeks later, when routine tasks have faded into the background. You stop thinking about the automation itself and simply notice that less busywork reaches your desk.
Hygiene by Design, Not Afterthought
True hygiene isn't something you bolt on at the end of a process; it's woven into the very fabric of how a space or product is conceived. When cleanliness is treated as a core design principle, surfaces become easier to reach, materials resist bacterial growth naturally, and workflow patterns discourage cross-contamination without relying on constant human vigilance. This shift from reactive sanitizing to inherent safety changes the entire relationship between people and their environment.
Consider the subtle differences that emerge when hygiene drives early decisions: seamless joins instead of grout lines that trap residue, drainage slopes calculated before a single fixture is placed, and airflows directed to keep contaminated particles away from clean zones. These aren't dramatic features you notice on a spec sheet—they're quiet, practical choices that reduce the daily friction of cleaning and make lapses far less dangerous. The result feels effortless because the hard thinking happened long before anyone picked up a disinfectant.
Retrofitting hygiene after the fact often means working against the grain of a design, adding barriers, signage, and extra steps that people eventually skip when rushed. By contrast, a hygienic-by-design approach aligns safety with natural behavior—sinks placed where hands get dirty, materials chosen to withstand frequent washing, and layouts that separate raw from ready-to-eat without requiring a checklist. That's the real measure of thoughtful design: not that it announces itself, but that staying clean becomes the path of least resistance.
Changeovers in Minutes, Not Hours
Waiting hours for a line changeover used to be considered normal in many production environments. Today, that assumption is being dismantled. Teams are rethinking setup procedures from the ground up, trimming internal tasks that once stopped machines for entire shifts. The result? Changeovers that happen in the time it takes to grab a coffee.
The shift isn’t about working faster under pressure. It’s about moving work outside the machine window, standardizing adjustments, and using visual cues that eliminate guesswork. One operator described it as “turning a marathon pit stop into a bicycle tire change.” The goal is simple: keep the line running, keep the schedule fluid, and let small batches become profitable.
When changeover time drops from hours to minutes, the entire production rhythm changes. You can respond to orders that arrive late, test new products without risking a full day of downtime, and finally treat setup as a controlled process instead of an interruption. Minutes aren't just a time measurement—they're a competitive edge.
Built-In Reliability and Support
Reliability here isn't a promise tacked on after launch—it's engineered into the flow of every update and every interaction. The system carries redundant safeguards by default, so a minor fault in one component triggers an automatic failover before you ever notice a slowdown. Logs and health metrics stay visible from a single dashboard, and built-in diagnostics flag potential issues with enough lead time to fix them during normal maintenance windows instead of scrambling at 3 a.m.
Support works alongside those built-in safeguards rather than replacing them. When you do need a human, the team responding already has the full context: your configuration, recent changes, and the exact failure path. That means fewer back-and-forth emails and more direct answers. We also keep a searchable internal knowledge base current with every release, so even self-guided fixes follow the same procedures our own engineers use.
What makes this different is the handoff between automated resilience and human help. Alerts don't just say "something broke"—they include the likely cause and the next step that was already attempted. If that step doesn't resolve the issue, a support ticket opens with that history attached. You're never starting from zero, and neither are we.
Efficiency Beyond the Spec Sheet
Real efficiency isn’t a single number printed next to a wattage rating. It’s how the machine behaves when the room temperature climbs, when the load shifts without warning, and when it has been running for six hours straight. The figures on a spec sheet are measured in clean, controlled conditions; actual work rarely happens there.
This is why attention goes to what cannot be captured in a brochure: transient response after a sudden demand spike, the heat dumped into a small enclosure, and the idle draw that quietly adds up over a month. These small behaviors shape daily experience more than a headline efficiency percentage ever will.
When you stop chasing the ideal number and start measuring what happens in your own environment, the difference becomes obvious. A device that holds steady under messy, unpredictable loads doesn’t just meet its specification. It earns its place.
FAQ
Look past the polished demo and check the frame construction, the quality of wear parts, and whether the manufacturer uses proven, off-the-shelf components for valves and seals. A machine built on a flimsy base or with proprietary parts will shake itself apart and leave you waiting weeks for replacements. Ask about mean time between failures on similar installations and, more importantly, ask to talk to a plant that has run the machine for at least two years.
Ignore the headline number and ask for the fill accuracy at your specific container size, product viscosity, and target speed. Run a trial with your actual product, not water, because foaming, particulates, and temperature all change the drip and cutoff behaviour. Then measure the standard deviation across a full hopper cycle, not just five consecutive fills. A machine that drifts as the tank empties will generate more giveaway than the spec sheet suggests.
In food, beverage, and pharmaceutical plants, changeover cleaning often takes longer than the filling run itself. Look for sloped surfaces, minimal flat areas, no exposed threads inside product contact zones, and quick-release guards. If the machine cannot be fully cleaned and inspected in under 30 minutes without tools, it will bottleneck production, especially for short runs. Also check whether the design supports clean-in-place cycles or at least tool-free disassembly for washdown.
If you need to switch between container sizes frequently or want to adjust fill profiles for delicate or foamy products, servo is worth the extra cost. Pneumatic systems are cheaper upfront but less repeatable at high speed and harder to dial in for gentle bottom-up filling. However, if you run one product at one speed all day, a well-built pneumatic filler can be perfectly adequate and far easier to maintain.
Do not buy a standalone filler if you have upstream depalletizers, cappers, or labelers. Look for native communication protocols such as EtherNet/IP or Profinet, and check whether the filler can share recipes and reject counts with line controllers. A machine with an open PLC means your own technicians can troubleshoot issues instead of paying for vendor service calls.
The wetted parts must handle your product chemistry, not just today's formulation. Stainless steel grade matters, with 316L preferred for acidic or salty products, but elastomers in seals and hoses need equal scrutiny. Some plastics degrade with certain preservatives or cleaning agents. Ask for a full wetted parts list, including seal compounds, and verify compatibility with both product and sanitizing chemicals.
Spare parts pricing, especially for wear items like nozzles and seals, can erase the initial savings. Also look at compressed air consumption, changeover labor, and whether the machine requires factory technicians for routine calibration. Energy and air usage are rarely on the spec sheet, but they show up monthly. Request a quote for recommended spare parts and a typical annual service contract before you commit.
It matters more than most people admit. If operators need a manual to adjust a fill volume or recover from a jam, you will lose time on every shift. Look for a touchscreen with role-based access, clear fault messages that tell you which sensor tripped, and one-touch recipe changes. The best interfaces let a new operator run the line safely within an hour, not after a week of shadowing.
Conclusion
Modern filling equipment rarely earns its keep through a single headline spec. What separates a machine that quietly improves margins from one that creates daily friction is how precision, automation, and hygiene work together. Look for fill accuracy that holds across viscosity shifts and container changes—not just on a lab-perfect demo run. The best systems pair that consistency with automation that operators actually trust: recipe-driven setup, clear fault diagnostics, and minimal need for manual overrides. At the same time, sanitary design should feel intentional. Sloped surfaces, tool-free guard removal, and crevice-free contact zones signal that cleaning was considered during engineering, not bolted on after the fact.
Beyond the build, pay attention to how quickly a line can pivot. A filler that takes a full shift to switch from one bottle size or product to another can erase the very gains it was bought to create. Look for toolless change parts, validated rinse-in-place cycles, and automatic positioning that reduces human error. Reliability is not just about uptime claims; it is about the manufacturer’s willingness to support the machine years after installation, with accessible parts, remote diagnostics, and clear maintenance schedules. Finally, judge efficiency by real-world output—gentle handling that reduces foam and waste, low compressed-air use, and repeatable rinse volumes—not just the maximum speed printed on a datasheet. The right modern filler is the one that stays easy to own after the initial purchase.
Contact Us
Contact Person: Tyson
Email: [email protected]
Tel/WhatsApp: +8613396971296
Website: https://www.wanyingmachinery.com