Stainless Steel D Shackle Supplier: What to Look for Before Buying
2026-10-18
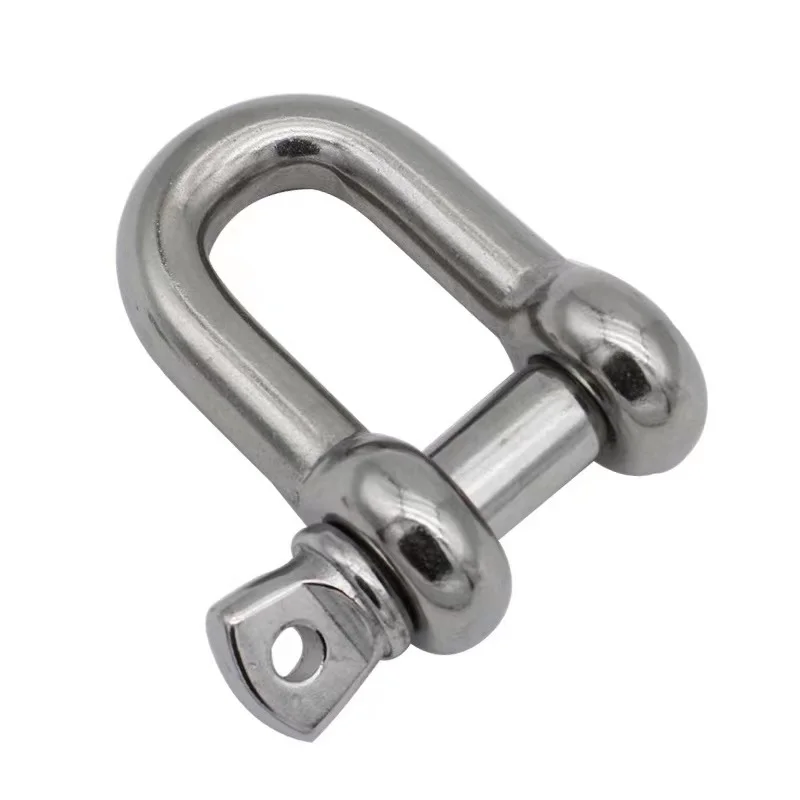
Every rigging component carries weight, but a stainless steel D shackle often bears the load when it matters most. Choosing the right supplier isn't just about price or availability—it's about trusting that the hardware won't fail under stress. Before you place an order, there are a few critical factors worth checking: material grade, load capacity markings, surface finish, and whether the manufacturer can back up their claims with testing. That last point is where many buyers get burned. If you're looking for a supplier that combines consistency with transparent quality control, Wanluo has built a reputation in this space. But let's break down what to look for before you commit.
Material Grade First: 304 vs. 316 Matters More Than You Think
Choosing 304 stainless steel often feels like the default move—it's widely available, costs less up front, and handles most indoor or mild environments without complaint. But that assumption falls apart the moment you deal with salt spray, chlorides, or even aggressive cleaning agents. In coastal kitchens, marine hardware, or swimming pool fittings, 304 can start showing rust spots within months, while 316 keeps its surface intact because of the added molybdenum. That single alloying difference quietly separates a part that lasts a decade from one that needs replacement in two years.
The price gap between 304 and 316 leads many buyers to optimize for the invoice rather than the lifecycle. You might save 20-30% on material costs today, only to discover pitting corrosion around welds or crevices later—especially where salt or bleach residue sits. 316 resists those localized attacks far better, which matters for anything that gets disassembled, sanitized, or exposed to humidity swings. In food processing and pharmaceutical lines, where downtime costs more than the metal itself, the upgrade isn't a luxury; it's basic risk management.
Ask any maintenance engineer who's dealt with a failed 304 bracket near a pool or a brewery floor drain, and they'll tell you the same thing: material grade decisions are made too early, usually by someone chasing a lower quote. Once the equipment is installed, swapping it out becomes far more expensive than the original savings. If your application involves chlorinated water, marine air, or harsh cleaning chemicals, start with 316. Leave 304 for indoor furniture, architectural trim in dry regions, or lightly loaded brackets where corrosion isn't a daily threat.
Working Load Limit: Don't Guess, Verify
The working load limit stamped on a sling or fitting isn't a suggestion—it's the maximum load the component can handle under ideal conditions. Guessing at this number, even when you're sure you've seen it before, is how accidents happen. Every piece of rigging has its own rating, and assuming one shackle matches another because they look alike is a fast track to failure. Take the time to actually read the tag, the stamp, or the documentation. If it's worn off or illegible, don't use the gear. Verification isn't optional; it's the only way to know the true capacity.
Start by locating the manufacturer's mark or tag on the equipment. For slings, the tag often includes the WLL, the type of hitch, and the angle factors. For hardware like hooks and rings, the load rating is usually forged into the metal. If you can't find a clear rating, treat the item as unrated and remove it from service. Don't rely on memory or similar-looking parts—different grades of chain or different alloys have vastly different limits. A quick check against the load chart and a visual inspection of the condition should be part of every lift plan.
The cost of guessing wrong is measured in dropped loads, damaged equipment, and serious injuries. A component that's overloaded by even ten percent can deform permanently, weakening it for future use. When in doubt, downgrade the lift, use a larger capacity component, or consult an engineer. No deadline is worth bypassing this step. Make verification a habit: before every lift, confirm the WLL of every item in the rigging assembly. It takes seconds, and it could save a life.
Surface Finish Is a Window into Manufacturing Quality
Surface finish isn't merely about how a part feels to the touch. It's a direct readout of the stability of the machining process, revealing minute vibrations, tool wear, and even inconsistencies in raw material. A dull insert leaves behind a torn, uneven texture, while a properly sharpened edge produces a crisp, uniform lay pattern.
Think of it as a fingerprint left by every operation that came before. Grinding, turning, milling, or honing each impose their own signature on the metal. When that signature drifts from the expected baseline, it signals something changed upstream—coolant concentration, spindle preload, or fixture rigidity. Skilled manufacturers don't just inspect for roughness values; they read the pattern to pinpoint the root cause.
This is why high-end aerospace and medical shops treat surface texture as a diagnostic layer, not a final checkbox. They measure Ra, Rz, and sometimes even bearing ratio, but the real value is in connecting those numbers back to process parameters. A consistent finish across thousands of parts is a quiet proof that the entire line is under control.
Certification Claims Need Proof, Not Promises
Too many certification programs lean on glossy promises about career acceleration or skill mastery without ever demonstrating how those outcomes are verified. A badge on a profile might signal completion, but it rarely shows the messy, unglamorous work of assessment—graded projects, proctored exams, or portfolio reviews by practitioners who actually do the job. If the only evidence is a certificate of attendance, the claim collapses under its own weight. Real credibility comes from transparent, third-party validation that can be inspected and challenged, not from a logo and a confident tagline.
Employers and clients have grown weary of credential inflation. They’ve seen too many candidates with identical lists of acronyms whose actual skills don’t match the marketing. That’s why proof matters more than promise: a link to a verified project repository, a recorded technical interview, or a rubric-scored assessment tells a story no brochure can. When certification bodies publish their evaluation criteria and allow results to be audited, the credential stops being a claim and becomes a record. Anything less is just a participation trophy dressed up as expertise.
The shift toward proof-based certification isn’t about being cynical—it’s about respecting the learner. If someone invests weeks in a program, they deserve to leave with evidence that can open doors on its own merits, not a document that requires a leap of faith from whoever reads it. Certification claims should be built on artifacts, not assurances. The moment a program can point to a specific, verifiable output and say “this is what competence looks like,” the promise becomes unnecessary.
Ask Where and How the Shackles Are Forged
Most people never stop to trace the chain back to the furnace. They feel the weight on their wrists, adjust their posture, and call it life. But the moment you ask where the shackles were forged, the question stops being philosophical and starts being practical. Was it a law written by strangers? A habit repeated until it felt like instinct? A story someone else told about who you are? The forge is rarely hidden; it's usually humming in plain sight, powered by fear, convenience, and the quiet need to belong.
Look closely at the making, not just the metal. Shackles aren't always hammered in a single blow. They are poured slowly, cooled in the water of daily compromises, then polished with the language of "that's just how it is." The forging happens in meetings where no one dares speak, in textbooks that skip certain pages, in the soft apology you give for wanting something different. Once you see the process, the iron loses some of its authority. You start noticing the joints, the weak welds, the places where a little sustained heat could warp the shape.
The harder question is how the shackles are forged inside you. External restrictions can be mapped, protested, or left behind. But the internal ones—the belief that you must earn rest, that conflict is always failure, that your worth is measured by output—those are cast in childhood kitchens and office hallways, then passed off as personality. Asking how they were made doesn't instantly free you. It does something rarer: it puts the hammer back where it belongs. In your own hand, not some unseen blacksmith's.
Custom Sizes and Markings Often Decide the Right Supplier
When sourcing components for specialized projects, the smallest dimensional tweak or a particular labeling requirement can quickly narrow your list of viable suppliers. A standard catalog part might seem economical at first glance, but hidden costs from retrofitting, additional machining, or manual rework often erase those savings. Suppliers who willingly adjust their production tooling for non-standard widths, lengths, or thicknesses—and who don't demand enormous minimum order quantities—tend to build stronger, longer-term relationships with buyers facing irregular specifications.
Markings present another layer of complexity. Whether you need laser-etched serial numbers, pad-printed logos, or ink-stamped batch codes that survive harsh environments, the supplier's in-house marking capabilities matter just as much as their core manufacturing precision. Outsourcing marking to a third party adds lead time, introduces quality-control gaps, and can create mismatched traceability records. The right supplier integrates marking directly into the production flow, verifying legibility and placement before parts leave the floor.
A practical way to evaluate a supplier is to request a small pre-production sample with your exact custom size and marking layout. Pay attention not only to whether they hit the spec but also to how they communicate about tolerances, setup fees, and repeatability. Suppliers that treat custom dimensions and markings as routine engineering challenges—rather than as inconvenient exceptions—almost always deliver smoother procurement cycles and fewer surprises in final assembly.
FAQ
For anything near saltwater, 316 or 316L is the safer bet. The added molybdenum makes a real difference against pitting. 304 can work for light-duty freshwater jobs, but I’d skip it for coastal or offshore use unless you enjoy replacing gear early.
Ask for the safety factor behind the rating. Reputable suppliers usually base their WLL on a 5:1 or 6:1 ratio to breaking strength. If they can’t tell you the breaking load or the factor, treat that as a warning sign. Also compare the WLL to similar shackles from known manufacturers—unusually high numbers often mean inflated claims.
Look for the WLL, size, material grade, and manufacturer’s mark stamped or lasered on the body. CE marking matters in Europe, but don’t rely on that alone. A trusted supplier will also be able to provide a certificate of conformity or a test report without you having to chase them.
Yes. Screw pins are fine for temporary rigging and quick changes, but a bolt-type pin with a nut and cotter gives better security when the shackle stays loaded or sees vibration. Check the thread engagement too—shallow or sloppy threads on a screw pin can strip under load.
Passivation should be standard after machining. If you need better performance, electropolishing removes more surface iron and leaves a smoother finish, which reduces places where salt can cling. Ask the supplier what they do after machining. If they don’t know or say nothing, that’s a problem for stainless.
Request a realistic lead time for a sample before you place a large order. Ask about their in-house machining capabilities versus outsourcing. A supplier who can explain how they adjust dimensions, pin tolerance, or thread specs is usually more dependable than one who just agrees to everything without detail.
In critical lifting or marine mooring, absolutely. Knowing which heat of steel your shackle came from makes failure investigations much easier and gives you leverage if a batch is defective. You don’t always need full mill certs for light-duty uses, but if the supplier refuses any traceability, I’d be cautious.
Conclusion
Before settling on a stainless steel D shackle supplier, it’s worth digging into the details that separate a dependable source from a risky one. The alloy choice is a prime example: 304 stainless handles general use, but if the shackles will face salt water, chemical exposure, or prolonged outdoor storage, 316’s molybdenum content makes a real difference in corrosion resistance. Never take a supplier’s word on working load limit—ask for the test data or at least clear marking on each shackle that matches the stated rating. A well-finished surface, free of pits, sharp edges, or uneven grinding, usually reflects careful forging and machining; if the finish looks rushed, the internal structure may be too. Likewise, certifications should be more than a logo on a brochure: request mill certificates, batch traceability, or third-party test reports that confirm the material and load rating claims.
Equally important is how and where the shackles are forged. A supplier who can explain the forging method—whether drop-forged, closed-die, or machined from bar—and who knows the origin of their stainless steel gives you a clearer picture of consistency and strength. Customization often reveals a supplier’s true capability. If you need nonstandard pin diameters, wider bows, or permanent markings like company initials or heat numbers, a flexible manufacturer with in-house tooling can save you from settling for off-the-shelf compromises. Instead of chasing the lowest quote, weigh these factors together: material grade, verified load limits, surface quality, proof of certification, forging transparency, and the ability to tailor sizes and markings. A supplier that welcomes these questions is far more likely to deliver shackles that hold up when it counts.
Contact Us
Contact Person: Shane
Email: [email protected]
Tel/WhatsApp: 8613357785029
Website: https://www.wanluohardware.com