RF Skin Tightening Machine Factory: A Complete Guide to Quality Manufacturing
2026-09-25
When sourcing RF skin tightening machines, most buyers focus on the price tag—but what really separates a reliable device from a costly mistake happens long before it ships. From coil winding to energy calibration, the manufacturing process quietly determines treatment efficacy, safety, and long-term durability. If you’ve been overwhelmed by vague supplier claims or inconsistent quality reports, this guide cuts through the noise. You’ll learn exactly what to look for inside a quality factory, how to verify production standards, and why Omeina has become a trusted name among clinics that refuse to compromise on performance.
The Part Sourcing Decisions That Determine How Long the Machine Survives
许多维修记录显示,机器提前报废很少是因为整机设计缺陷,而是某个不起眼的零件先失效,随后引发连锁损坏。采购时如果只比较单价和交货期,忽略了材料等级、热处理工艺或密封件硬度,设备寿命可能从设计目标直接砍半。例如,一个用于粉尘环境的轴承,若选用了不带接触式密封的普通型号,润滑脂会在几周内被污染,磨损速度远超预期。
供应商的批次稳定性同样致命。同一张图纸,不同工厂做出来的齿轮或轴套,可能在表面粗糙度和残余应力上存在差异,而这些差异会在高周疲劳中逐渐放大。有些采购团队习惯在合格供应商名单里轮流下单,却从不核对每批零件的金相报告或尺寸检测数据。结果就是性能时好时坏,故障间隔时间波动很大,维护团队只能不断救火。
真正能延长机器寿命的采购决策,往往是把钱花在少数几个关键零件上。识别出那些一旦失效就会导致停机或安全风险的部件,对它们执行更严格的来源控制,甚至要求供应商提供批次可追溯的材质证明。同时,把每次故障的零件批次、使用时长和失效模式记录下来,反过来调整采购标准。这种闭环会让采购从单纯的砍价角色变成设备可靠性的第一道防线。
Calibration Routines That Keep Energy Output Predictable
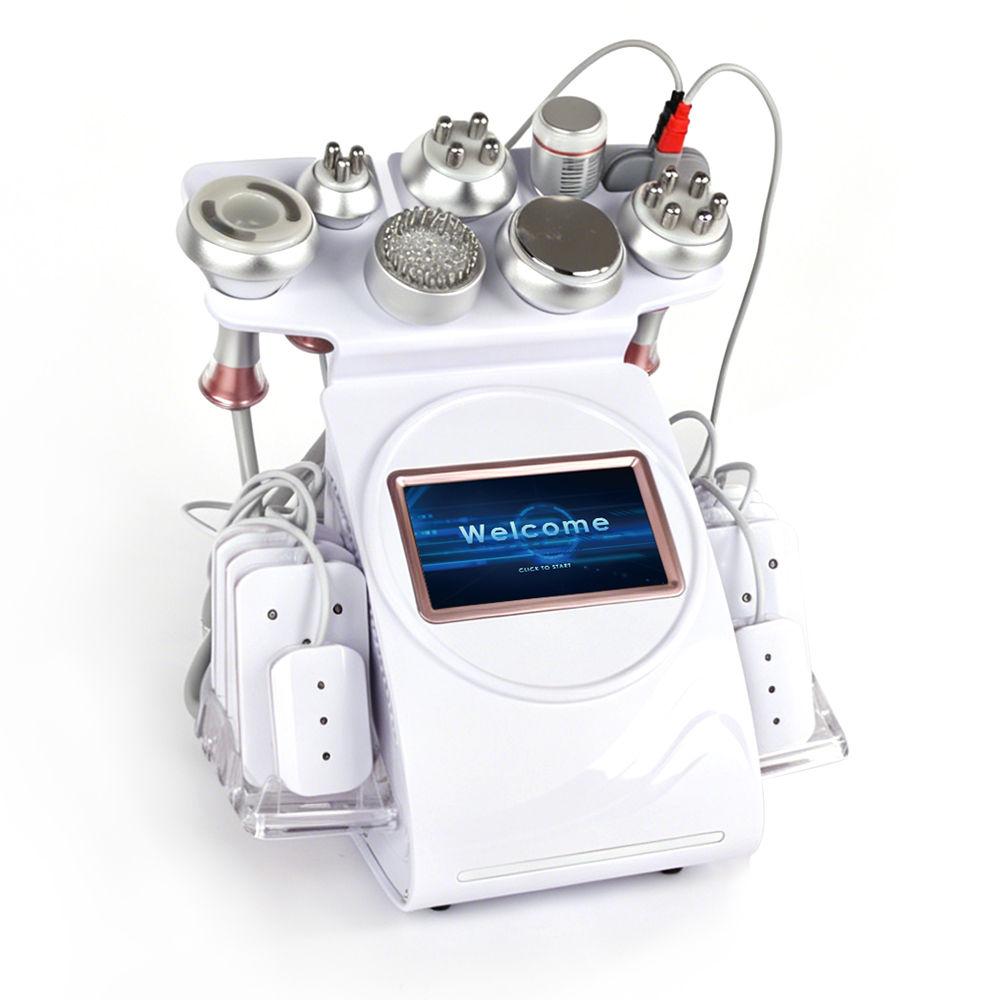
Regular calibration isn't just a maintenance checkbox—it's the buffer between a smooth operation and a cascade of guesswork. When energy output drifts even a few percent, downstream decisions start compounding errors. A solid routine anchors the system to a known reference, so the numbers you see reflect reality rather than a slowly shifting assumption.
The most useful routines are built around fixed intervals and clear trigger points. Weekly zero-point checks catch early drift before it becomes a pattern. Monthly load-bank tests push the system across its operating range, revealing nonlinearities that only show up under stress. And after any hardware swap or firmware update, an immediate re-calibration closes the loop—otherwise you're trusting a new component with old offsets.
What separates predictable output from constant firefighting is documenting the routine without letting it become ritual. Record not just the adjustment values but the ambient conditions, warm-up time, and any recent changes. Over months, that log becomes a diagnostic map: you'll spot seasonal shifts, aging sensors, or a subtle power-supply ripple before they ever show up as an outage.
Where Assembly Lines Cut Corners—and How to Spot It
Most line-side shortcuts aren't dramatic failures—they're quiet substitutions that pass a quick glance but degrade over time. The first place to look is fastener torque: many plants dial back pneumatic clutch settings to speed cycle time, leaving bolts a half-turn shy of spec. You won't see it on a stationary vehicle, but after a few thousand miles of vibration, panels start to chatter and brackets work loose. Another common trim is seam sealer application. Instead of a continuous bead, you'll find skipped sections or a thinner-than-specified layer behind trim pieces, which invites moisture into pinch welds and accelerates rust in areas that never see direct sunlight.
Welding is where the most dangerous cost-cutting hides. Robotic cells can be reprogrammed to reduce the number of spot welds per inch on non-structural flanges, or to use shorter weld times that leave cold spots under a cosmetic surface. On a finished product, run your finger along a door sill or under the hood lip—if the weld indentation feels inconsistent in depth or spacing, it's a red flag. Similarly, paint prep often gets shortened: phosphate baths run at lower concentration, or rinse stages are skipped entirely. Within a year, you'll see micro-blistering at the edges of rocker panels and behind wheel arches, where adhesion was never properly established.
Spotting these shortcuts after delivery comes down to pattern recognition. Use a flashlight at a low angle across body panels to reveal waviness that indicates skipped sanding or thin filler. Check for asymmetrical gaps around doors and fenders—not just width, but consistency along the entire shut line. And don't ignore smell: a properly cured interior shouldn't off-gas a sharp solvent odor after a week in the sun, which points to skipped post-bake ventilation or cheaper adhesives. If you notice two or three of these signs on one vehicle, assume the line was chasing cycle time rather than durability, and inspect the safety-critical areas twice.
Stress Tests That Simulate Years of Daily Use in a Week
Most products don't fail on day one—they die slowly, after thousands of small interactions. A backpack zipper gets tugged twice a day, a laptop hinge opens and closes dozens of times, a chair armrest gets leaned on every afternoon. To understand how something holds up over five or ten years, test engineers compress that entire timeline into a single week. The math is simple: if a part is expected to survive 50,000 cycles in the real world, a servo-driven rig can run those 50,000 cycles nonstop over six days, pausing only for inspections and lubricant checks.
The machines themselves aren't glamorous—pneumatic pistons, rotating drums, heated chambers, salt-spray nozzles—but they're relentless. A button gets pressed by a metal finger 80 times a minute, hour after hour, until it reaches 300,000 actuations. A zipper is yanked open and shut under a 10-pound load for 20,000 cycles while dust is blown into the teeth. Fabrics are rubbed against a standard wool abrasive for 40,000 rotations to mimic years of sleeves dragging across desks. Meanwhile, separate samples sit in environmental chambers that swing from -20°C to 70°C with 90% humidity, because thermal expansion and moisture do as much damage as physical wear.
After the torture ends, engineers don't just look for catastrophic breakage. They measure how much force the button now requires, whether the zipper still aligns within 0.3 millimeters, if the fabric has pilled beyond an acceptable grade, and whether any plastic has become brittle from UV exposure. A product passes only if it remains fully functional and visually acceptable after the equivalent of years of daily use. The failures that do slip through are rare, and when they happen, the test data points straight to the weak spot—sometimes a tiny change in material thickness or a different coating is all it takes to turn a six-day failure into a ten-year product.
Custom Orders Done Right: Balancing Flexibility and Lead Times
Custom orders often feel like a gamble. Clients want a product tailored to their exact specifications, but they rarely want to hear that the lead time will double. The key isn't to offer unlimited flexibility or rigid constraints; it's to define a clear boundary where customization adds value without collapsing your production schedule. For instance, allowing customers to choose from a verified set of materials or finishes keeps the process nimble, while still giving them a sense of ownership. Communicate these options upfront, and pair each choice with a realistic time frame. That way, a bespoke request doesn't quietly become a bottleneck.
One underused tactic is to segment custom work by complexity. A simple modification—like a different thread color or an engraved name—can be slotted into standard production with minimal delay, often just a day or two. More involved changes, such as altered dimensions or structural redesigns, get a separate queue with a longer, clearly stated lead time. This approach prevents the common mistake of treating every custom order as a one-off project. Instead, you create a predictable flow: small tweaks stay fast, major overhauls get the time they actually need.
Finally, don't hide the trade-off. Customers respect honesty more than a rushed promise that falls apart later. When you present a custom option, explicitly say: "This adds three business days" or "This moves your order to the custom batch, which ships in two weeks." Back that up with a simple status update system, so the buyer always knows where their order sits. Balancing flexibility and lead times isn't about saying no—it's about giving customers a menu of choices where each one comes with a clear price in time, not just money.
The Paper Trail: Why Documentation Matters More Than You Think
Most people treat documentation as a chore—something to rush through after the real work is done. That illusion shatters the first time a disagreement escalates or a key team member walks out the door. A written record turns fuzzy recollections into something you can actually point to, whether it’s a change order on a construction site or a quiet note about why a software patch got rolled back at 2 a.m.
The real value isn’t the file itself; it’s the thinking it forces you to do. Writing down what happened and why exposes holes in your own logic before someone else finds them. A well-kept trail lets you trace a decision back to its source, which sounds boring until you’re sitting in a courtroom or a postmortem meeting wishing you had one.
FAQ
Look closely at how they manage the RF energy delivery path. A quality factory will use medical-grade capacitors and custom inductors rather than off-the-shelf parts, and they'll calibrate every machine against a known tissue phantom before shipping. You should also ask about their soldering standards for high-frequency traces — sloppy joints cause hot spots that damage skin. If the factory can't show you photos of their calibration bench and trace inspection process, keep looking.
Request a live video walkthrough of the production floor, not a polished brochure. Ask to see the SMT line, the specific jigs used for handpiece assembly, and the testing station where they measure output frequency and impedance matching. A real factory will have a partially assembled unit on the bench and can name the suppliers of their main chips. If they hesitate or offer only stock photos, that's a red flag.
For most markets, you want ISO 13485 for medical device quality management, plus CE marking if selling in Europe, and FDA registration or clearance if targeting the US. Don't just accept a certificate at face value — verify the number on the issuing body's database. Some factories show outdated or suspended certificates, so ask for a recent audit report summary. RoHS compliance matters too, because it indicates they control hazardous substances in the handpiece and cables.
Every unit should undergo a burn-in test of at least four hours running at maximum output, with the handpiece attached to a load that simulates skin resistance. After that, they should measure the actual RF frequency, output power stability, and surface temperature of the handpiece tip under controlled conditions. A good factory keeps records for each serial number, so you can trace any field failure back to a specific test log. Ask to see a sample log — blank or generic entries indicate sloppy QA.
Ask about the cable strain relief design, the connector plating thickness, and how they test the handpiece's repeated flexing. Cheap factories use thin gold flash on connectors that wears off after a few hundred insertions, causing intermittent power drops. A reliable factory will have a dedicated tester that bends the cable thousands of times while monitoring output. Also ask what replacement handpiece price they offer — if it's below $50, the internal electrodes are probably not durable or safe for repeated treatments.
The biggest one is unstable RF output that drifts as the machine heats up, so the first few clients get good results and later ones get no effect or even burns. Another is unsealed handpiece tips that trap gel and skin oils, causing corrosion inside. Also watch for mismatched power adapters that work in the factory but fail on your voltage, or unshielded cables that interfere with other salon equipment. These issues rarely show in marketing materials but come up constantly in field service.
A good factory will have a configuration file or small software utility to change the startup logo, treatment presets, and language. They should offer this without changing the core firmware, because each firmware change needs re-validation for safety. Ask if they can pre-set your clinic's protocol names and time intervals before shipping. If a factory says 'any customization is easy' but can't explain the difference between a parameter change and a firmware change, they're likely to delay your order or ship a buggy unit.
Look for a factory that assigns an engineer, not just a salesperson, to your account. They should provide a service manual with schematics, not just a user manual. When you report a fault, they should ask for specific measurements like 'what is the voltage at test point TP3' rather than immediately suggesting you ship the unit back. Fast spare parts dispatch — ideally from a local warehouse — and a written warranty that covers the handpiece for at least one year also separate serious manufacturers from box-movers.
Conclusion
In a market flooded with devices that look nearly identical on the outside, the real story of an RF skin tightening machine's longevity is written in the sourcing choices made long before the first panel is screwed on. Factories that prioritize durable capacitors, medical-grade power supplies, and hand-soldered connections over cheap wave-soldered boards produce units that routinely outlast their warranties by years. But parts alone don't guarantee consistent results. Calibration routines—ideally performed on every single unit after a 48-hour burn-in cycle—are what keep energy output within a tight tolerance, so the tenth client of the day feels the same warmth as the first. And while most buyers never visit the floor, knowing where assembly lines cut corners matters: look for unevenly applied thermal paste, mismatched screw torques, or cables that are zip-tied instead of routed through dedicated channels. These are quiet signals that quality control was an afterthought.
The factories worth trusting are the ones that don't just build machines—they torture them. A proper stress test doesn't just run the device for a few hours; it cycles the handpiece through hundreds of rapid temperature swings, simulates drops onto concrete from waist height, and runs the RF generator at 110% of rated output for days. This compression of years of daily use into a single week reveals solder joints that will crack and capacitors that will drift before they ever reach a clinic. Custom orders add another layer of complexity: the best factories balance flexibility with honest lead times, refusing to promise a 10-day turnaround on a bespoke interface when they know it needs 21. Finally, documentation is the thread that holds everything together. A factory that provides full BOMs, calibration logs, and batch-level test reports isn't just being bureaucratic—it's giving you the paper trail needed to trace a field failure back to a single reel of resistors, which is the difference between a recall and a fix.
Contact Us
Contact Person: Tina Liu
Email: [email protected]
Tel/WhatsApp: 8618681405932
Website: https://www.omeinabeauty.com/