PVC Antistatic Flooring Exporter Insights for Choosing the Best Anti-Static Flooring System
2026-09-16
Choosing the right anti-static flooring is about more than meeting a spec sheet—it’s about protecting sensitive equipment, preventing costly downtime, and ensuring long-term durability. Drawing on years of experience as a PVC antistatic flooring exporter, Lipin Floor shares the practical insights that most generic guides miss. From material composition to installation nuances, this post breaks down what actually matters when selecting an anti-static flooring system that will hold up in demanding environments.
Static Dissipation Starts With the Right PVC Layer, Not the Thickest One
很多人以为,只要把PVC层做得足够厚,静电问题就能迎刃而解。但实际测试数据往往给出相反的结论:静电消散效率取决于材料内部的导电网络是否连续,而不是单纯的体积堆砌。一层薄而均匀的改性PVC,远比一层厚却缺乏导电填料的普通PVC更可靠。
关键在于配方中的碳黑、金属纤维或离子型抗静电剂如何分布。这些导电介质需要在PVC基体中形成有效的渗透路径,让电荷能够快速迁移到接地端。如果厚度增加但导电网络稀疏,电荷反而会在绝缘区域积累,最终以火花形式释放——这正是我们需要避免的。
因此,选择静电耗散材料时,别被“厚度即性能”的直觉带偏。先确认PVC层的表面电阻率是否稳定在10^6到10^9欧姆区间,再考虑机械强度所需的厚度。正确的材料搭配接地设计,才能让静电在产生之前就被安全导走。
Resistance Ranges That Make Sense for Electronics Assembly Versus Warehouses
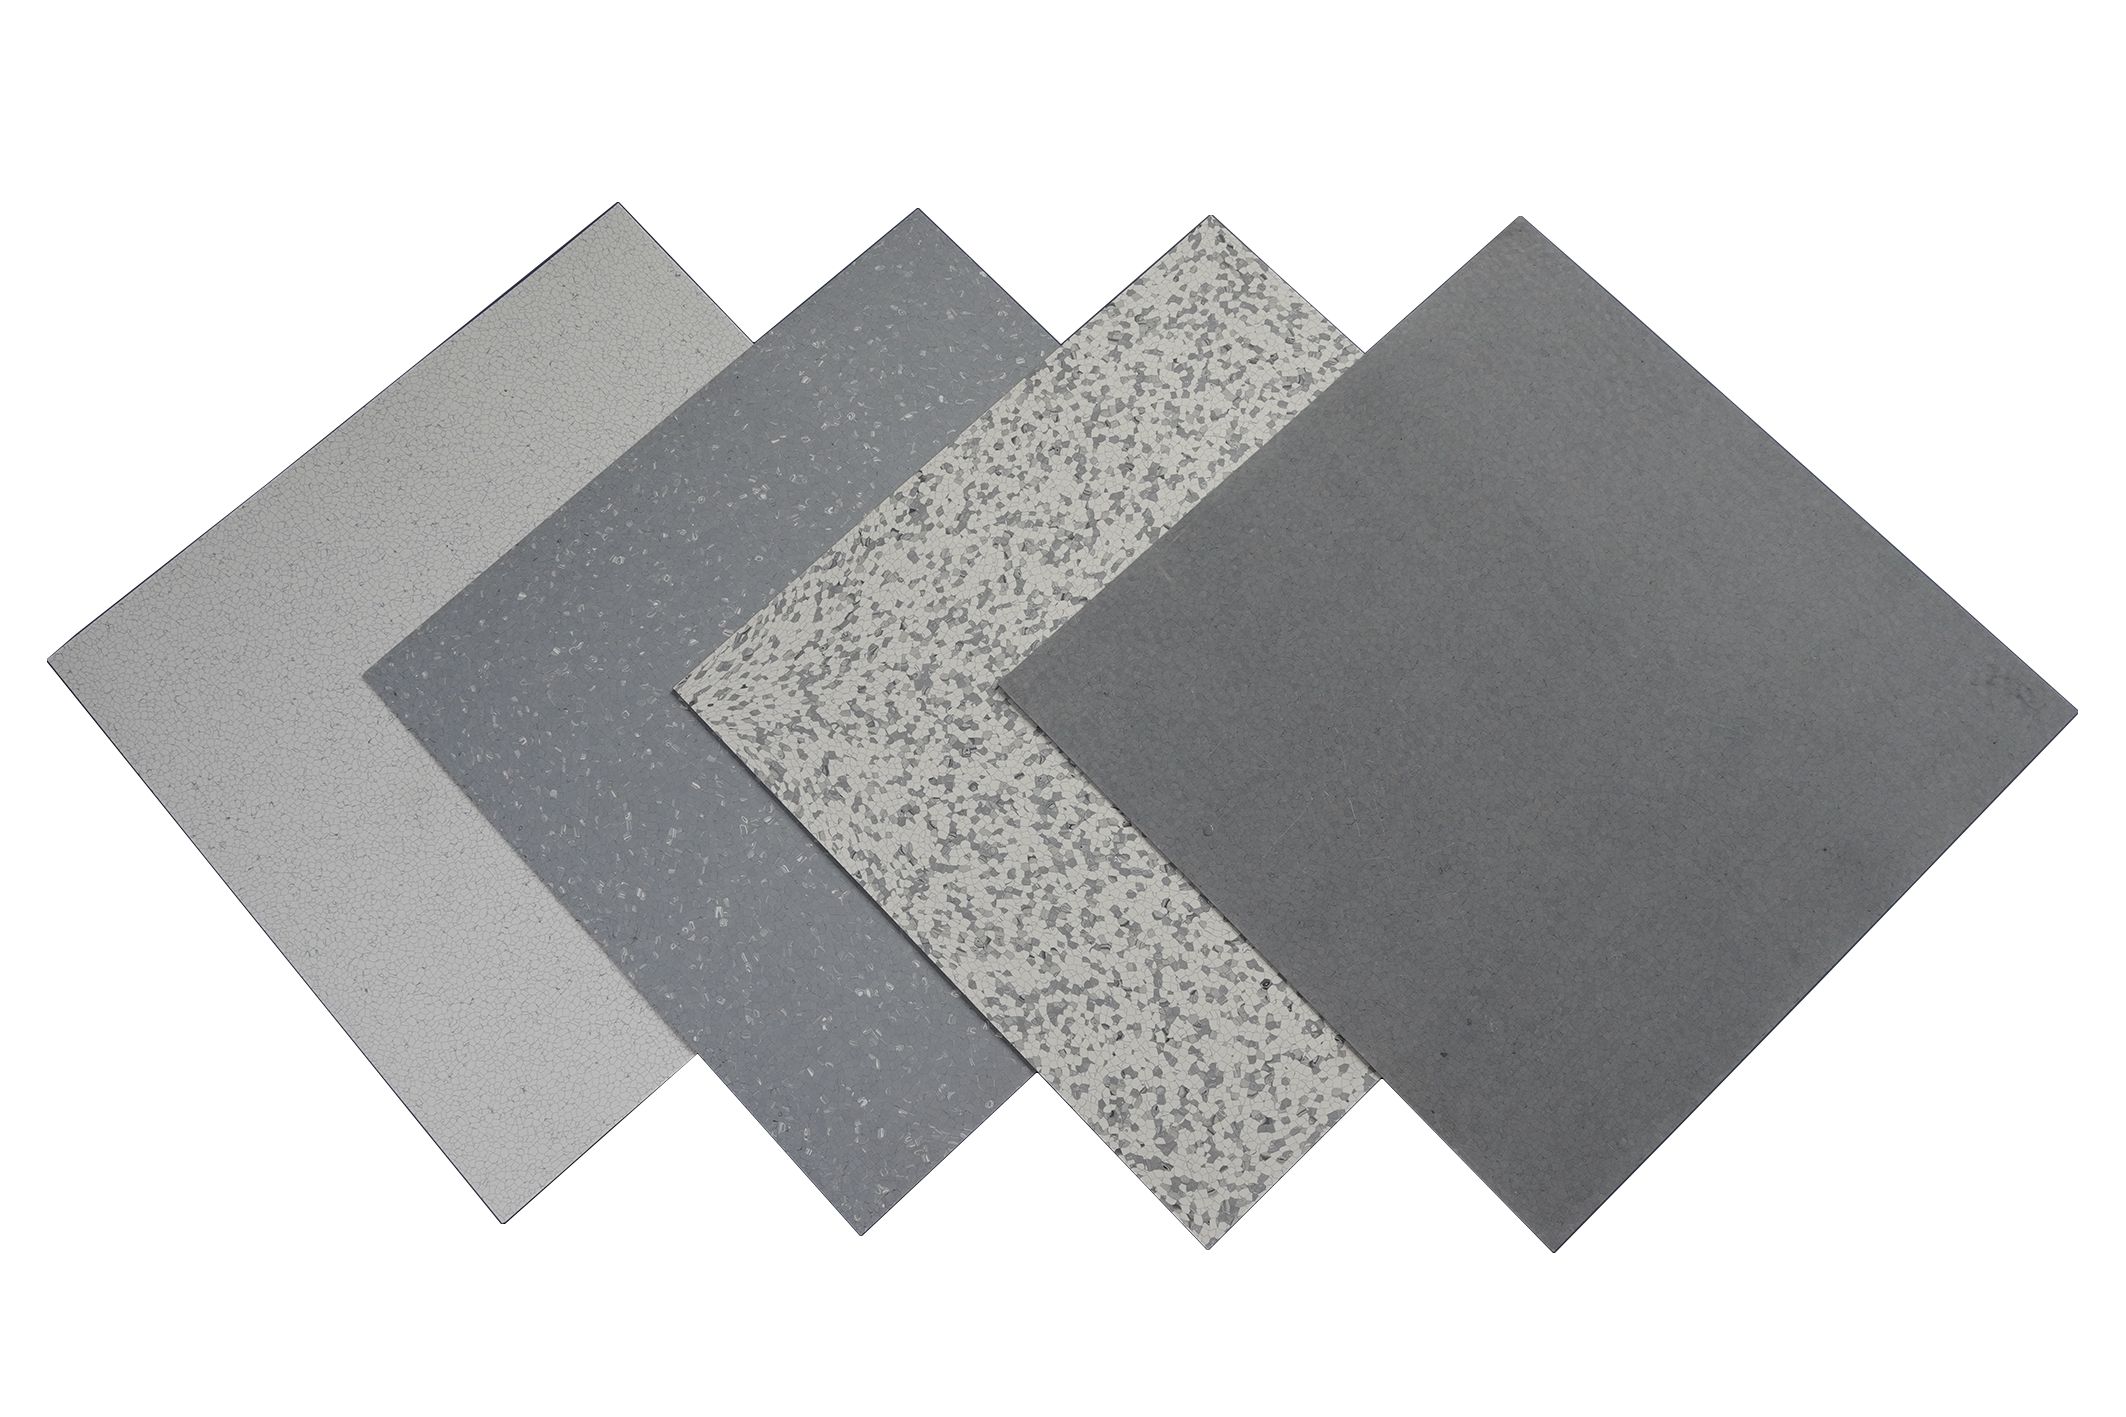
For electronics assembly areas, resistance ranges need to sit low enough to bleed off charges before they can zap sensitive components. A floor measuring between 1 x 10^6 and 1 x 10^9 ohms point-to-point is typically the sweet spot—dissipative enough to drain static quickly, but not so conductive that it creates a safety hazard for workers near live equipment. In practice, many fabs and assembly benches aim for the lower half of that band, often under 1 x 10^8 ohms, because even small residual voltages can damage modern ICs. Testing with a megohmmeter at 100V will show whether the floor stays in range after wear, cleaning, and humidity swings.
Warehouses, by contrast, don't need the same aggressive dissipation. Most warehouse operations deal with packaged goods, pallets, and occasional hand tools—not bare boards or microchips. A resistance range of 1 x 10^7 to under 1 x 10^10 ohms is usually plenty to prevent nuisance shocks and avoid attracting dust, while still protecting any packaged electronics from gross static buildup. Going too low in a warehouse can actually create problems: conductive floors may require special grounding and can interfere with forklift battery charging areas, plus they cost more without adding real benefit.
So the practical split is: electronics assembly floors should be tested and maintained at 1 x 10^6–1 x 10^9 ohms with a bias toward the lower end, while warehouses can accept 1 x 10^7–1 x 10^10 ohms without compromising safety or product integrity. Matching the resistance to the actual handling activity prevents over-engineering and keeps maintenance straightforward.
Why Grounding Grids Work Better When the Adhesive Is Also Considered
Most grounding grid installations focus heavily on conductor material, mesh spacing, and soil resistivity, but the interface between the grid and the underlying surface rarely gets the same attention. Without a proper adhesive, even a well-designed grid can leave microscopic air pockets at the contact points, driving up local contact resistance. A conductive adhesive fills those gaps completely, creating a continuous electrical path that would otherwise rely on pressure alone. This single change often drops the overall ground resistance by a noticeable margin, especially in dry or rocky soils where natural contact is poor.
Beyond electrical performance, adhesives solve a mechanical problem that is easy to overlook. Grounding grids buried under soil or concrete can shift over time due to thermal expansion, moisture cycles, or minor ground movement. When the grid loses firm contact with the surrounding material, its effectiveness degrades silently. A well-chosen adhesive locks the conductors in place, preventing micro-movements that lead to corrosion and loose connections. This is particularly valuable in areas with freeze-thaw cycles or high vibration, where a rigid bond keeps the grid performing as intended year after year.
The type of adhesive matters as much as the decision to use one. Conductive epoxies and carbon-loaded compounds are common choices, but they must be compatible with both the grid material and the surrounding environment. In damp locations, a moisture-resistant adhesive prevents galvanic corrosion that would otherwise eat away at the copper or steel. In high-temperature settings, an adhesive with a matching thermal expansion coefficient avoids cracking. The point is not simply to glue the grid down, but to treat the adhesive as part of the electrical system—carefully selected and applied, it turns a decent grounding grid into a consistently low-resistance path that holds up under real-world conditions.
Reading Between the Lines of Wear Resistance and Real Foot Traffic
Lab tests will tell you a floor can survive ten thousand passes with a mechanical abrasion wheel, but they won't mention that a stroller with a stuck wheel or a delivery cart dragged sideways will chew through the surface in a month. The real story hides in the unglamorous corners: entry mats that catch half the grit, bar stools that pivot on one leg, the exact spot where a queue forms every morning. If you only look at the wear rating, you miss the fact that most damage happens in the first three feet inside a door, where sand and moisture act like sandpaper long before the rest of the room sees any traffic.
Contractors love to quote the number of cycles a product survived in a controlled chamber, but on-site observation tells a different tale. A restaurant floor might fail not because the material is weak, but because the weekly cleaning crew uses the wrong pH and strips the protective layer faster than footfall ever could. A hotel corridor with the same polished concrete will show zero wear near the windows—nobody walks there—and a dull, scratched path right down the middle where luggage wheels have carved a groove. Wear resistance means nothing unless you map how people actually move, pause, pivot, and drag things across the surface.
If you want to design for foot traffic, you have to stop trusting the spec sheet and start counting scuff marks. Watch where the barista stands for eight hours; see how the rubber sole of a work boot grinds against the edge of a stair tread. Those micro-interactions never show up in an abrasion test. The real measure is whether a floor can shrug off a year of Tuesday-morning deliveries and still look intentional—not just intact. That is the gap between a lab number and a lived-in surface, and it is where most material choices quietly fail.
Export-Spec Tolerances That Affect On-Site Performance
When a component leaves the factory with a tolerance that looks reasonable on paper, the real test happens once it meets the uneven floors, temperature swings, and installation quirks of an actual job site. A shaft diameter held within ±0.05 mm might pass a bench check, yet bind against a mating bore after both pieces have sat in the sun for an hour. Export-spec tolerances often ignore this kind of thermal drift because the original test environment never accounted for a container crossing the equator.
The gap between drawing and delivery becomes obvious in fastening patterns. Holes drilled to export tolerance may align perfectly with a fixture jig, but the moment a technician uses a hand drill on a slightly warped mounting plate, the cumulative error doubles. What was meant to be a slip fit becomes a forced interference, and the on-site team compensates with shims, reaming, or outright modification — erasing the precision the spec promised. This is rarely a flaw in the tolerance itself; it is a failure to connect that tolerance to the messy reality of field assembly.
A better approach is to treat export tolerances as a starting point, not a guarantee. Build in a little breathing room for thermal expansion, tool misalignment, and surface contamination. Then test the final assembly under conditions that mimic the destination site: uneven support, hand-tool torque, and temperature cycles. Only then will the numbers on the export drawing hold up when the equipment is finally bolted into place and expected to run without complaint.
Cleaning Routines That Keep Anti-Static Properties From Fading
Most anti-static clothing loses its effectiveness because of what happens in the wash, not from normal wear. Flip garments inside out before washing, stick with cool or lukewarm water, and use a mild, pH-neutral detergent. Fabric softeners and dryer sheets are the usual culprits here—they leave an insulating film on the fibers that can quiet the conductive threads meant to keep static in check.
For spot cleaning, skip the rough washcloth and use a microfiber cloth or soft sponge with a tiny bit of diluted detergent. Pat the area instead of scrubbing, since friction damages the carbon or metal fibers that carry charge away. Let the item air dry flat or on a padded hanger, out of direct sunlight and away from radiators. If you must use a dryer, choose the lowest heat setting and pull the garment out while it is still slightly damp.
Every few washes, a plain cool-water rinse with a splash of white vinegar can strip away detergent buildup without attacking the anti-static finish. Just do not do this every time—vinegar is mild, but repeated acids can weaken some treatments. After it dries, test the garment by rubbing it against a clean cotton cloth; if it still clings, it is usually time for a gentle reapplication rather than a stronger wash cycle.
FAQ
Many buyers focus on the quoted price and skip the batch-to-batch consistency data. Ask for surface resistance test results from three separate production runs, not just a single sample. Also check whether the conductive filler is evenly distributed across the full tile thickness, because some exporters only add carbon or graphite to the top layer, which leads to dead spots after wear.
Low humidity weakens conductivity because there is less moisture to help dissipate static. A reliable PVC system should be tested at 12% relative humidity, not just at 50%. Request test reports that list resistance values at low RH, and make sure the flooring uses conductive fillers that do not depend on ambient moisture.
Not necessarily. A thicker wear layer can protect the pattern, but if the conductive layer sits deeper, surface resistance may rise. For electronics assembly areas, a thinner clear wear layer over a properly loaded conductive core often gives more stable static dissipation than a thick decorative layer with marginal conductivity.
The copper strip placement and connection points matter more than many buyers expect. Each tile should connect to copper tape in at least two places, and the tape grid needs to link to a verified earth ground. Without a proper grounding schedule, even a highly conductive PVC tile will not drain charge from a person or cart.
Static-dissipative flooring with surface resistance between 10^6 and 10^9 ohms is usually safer for server rooms. It drains charge slowly enough to avoid a sudden discharge into sensitive equipment. Conductive flooring below 10^6 ohms may be needed for explosive handling areas, but it can create a shock hazard if someone touches a live circuit.
Look at the cost per square meter per year of stable performance. Include the expected wear life of the conductive layer, cleaning chemical compatibility, and whether the resistance drifts after repeated buffing. A cheap system that loses static control after two years of traffic costs more than a mid-priced tile with stable resistance for ten.
Lab tests often measure a new, clean sample under ideal humidity. On site, joints open, copper tape lifts, or housekeeping uses a wax finish that insulates the surface. Ask the exporter for field failure examples and their recommended maintenance routine; a supplier who only shares lab certificates is not telling you how the floor behaves after installation.
Conclusion
Too many buyers still equate a thicker PVC wear layer with better static control, but that assumption quietly undermines an entire installation. The dissipative performance begins in the PVC compound itself—carbon or graphite particles must form a consistent conductive network, and a thinner, well-formulated layer often outperforms a thicker one loaded with the wrong filler. Equally important is matching the resistance range to the actual space: electronics assembly and sensitive component handling typically demand a tighter range, while warehouses with forklifts and pallet movement can tolerate a broader window without sacrificing safety. A grounding grid, no matter how carefully laid, loses its value if the adhesive beneath the flooring acts as an insulator. Conductive adhesives complete the circuit, and skipping that detail turns a static-control floor into a decorative one.
Wear resistance claims can mislead unless they are read against real foot traffic patterns, including rolling loads and abrasive dust, not just laboratory abrasion tests. Export-spec tolerances also matter once the product leaves the factory: thickness, flatness, and resistance values can shift with temperature and humidity during shipping, so a floor that passed in one climate may behave differently on site. Finally, anti-static properties fade fastest when cleaning routines are ignored. Using the wrong wax or aggressive detergent leaves an insulating film, while proper pH-neutral cleaners and regular conductivity testing keep the system functional for years. Choosing the best anti-static PVC floor is not about chasing a single spec; it is about aligning material chemistry, installation details, and maintenance from day one.
Contact Us
Contact Person: yuki
Email: [email protected]
Tel/WhatsApp: +86 18664390732
Website: https://www.lipinfloor.com/