PTFE Gland Packing Exporter: Your Trusted Source for Superior Sealing Solutions
2026-10-15
Leakage is rarely a sudden failure—it starts with the wrong packing choice. For maintenance teams handling aggressive chemicals, high pressures, or frequent thermal cycling, a standard gland packing often falls short. That's where a specialized PTFE gland packing exporter like TAIFNO changes the equation. Instead of settling for off-the-shelf products, you get sealing solutions tailored to real operating conditions. In this guide, we'll break down what to look for in PTFE gland packing and why TAIFNO has become a go-to source for plants that can't afford unplanned downtime.
How PTFE Gland Packing Keeps Aggressive Fluids Where They Belong
PTFE gland packing earns its reputation the moment a maintenance crew unwraps it. The material’s near-zero friction surface lets the rings slide against a shaft without carving grooves, while its chemical inertness holds up against acids, caustics, and solvents that would chew through graphite or aramid in a matter of weeks. That combination means the seal isn’t just tight—it stays tight, even when the pump cycles through start-stop abuse.
Much of the staying power comes down to how the packing is installed and compressed. A proper gland follower load spreads through the braided structure, forcing the PTFE to flow just enough into the stuffing box’s microscopic gaps. Unlike softer packings that need constant re-torquing as they relax, PTFE holds its set under temperature swings, so the leak path that usually opens up after a few thermal cycles never gets a chance to form.
If you’re dealing with aggressive media, the real story is longevity. A well-fitted PTFE gland packing can run for months without a drip, not because it’s overtightened, but because the material resists both chemical attack and cold flow. That’s what keeps the aggressive fluid on the process side—right where it belongs.
Braided to Handle Heat, Pressure, and Constant Motion
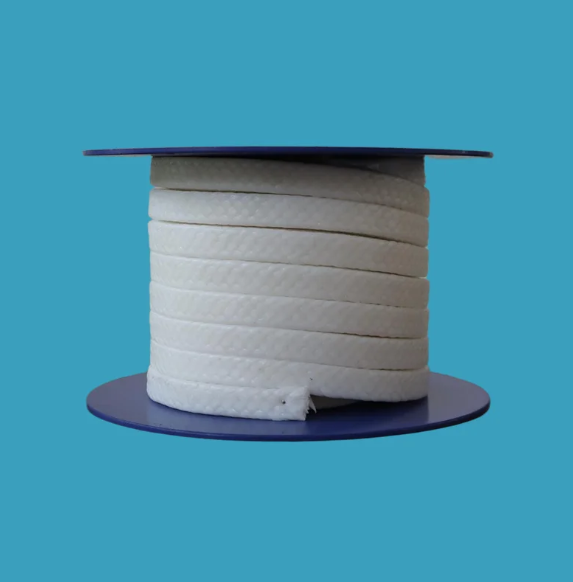
The braided construction isn't just for looks. Each strand interlocks with the next, distributing stress evenly across the entire length. When heat builds up, the weave allows for micro-expansion without cracking or stiffening. It's the same principle behind a steel cable on a suspension bridge, scaled down to something you can hold in your hand.
Under pressure, ordinary materials buckle or deform. This braid holds its shape because the tension from every angle cancels out weak points. Twist it, bend it, run it through a tight radius, and the core stays protected. Constant motion only tightens the interlock, so the more you use it, the more it settles into a reliable, wear-resistant shell.
Think about environments where vibration never stops, where temperature swings from freezing to scorching in minutes, and where a single point of failure isn't an option. That's where a braided design earns its keep. No seams to split, no layers to peel apart. It absorbs the punishment and keeps transmitting, conducting, or flexing exactly as it should.
Choosing the Right Cross-Section for Pumps, Valves, and Mixers
Engineers often treat a component's cross-section as a simple geometric afterthought, but in fluid-handling equipment it quietly dictates everything from pressure drop to fouling resistance. A pump impeller vane with a blunt, circular profile might survive abrasive slurries, yet the same shape in a high-speed clean-fluid valve creates unnecessary turbulence and erosion. Matching the section to the operating reality means weighing three things at once: the flow regime, the aggressiveness of the media, and the maintenance window you can honestly tolerate. Start by mapping where velocity gradients will be steepest, because that is exactly where a poorly chosen profile turns into a recurring failure point.
For valves, the argument rarely ends at round versus rectangular. A rounded interior passage softens sudden expansions and contractions, reducing cavitation noise, but it can also trap solids in the dead zones behind the seat. Conversely, a sharp-edged or wedge-shaped cross-section self-cleans with every cycle, yet it invites stress concentrations at the corners. The practical compromise often lies in an asymmetric profile: steep on the upstream side to accelerate flow deliberately, gently tapered downstream to recover pressure without separation. This asymmetry is what separates a valve that lasts five years from one that needs seat replacement every quarter.
Mixers add another layer because the cross-section directly affects both shear and blend time. A wide, flat blade cross-section moves a large volume but creates a cavern of slow-moving material around the shaft, while a narrow, steeply pitched section drives local turbulence that may or may not reach the vessel wall. Testing multiple profiles in a transparent mock-up is far cheaper than discovering a dead zone in a production batch. When in doubt, choose a section that fails safe: one that encourages gradual wear rather than sudden fracture, and that can be inspected without dismantling the entire rotating assembly.
Custom Lengths and Blends That Fit Your Existing Equipment
Most suppliers hand you a catalog and expect your production line to adapt. We take the opposite approach. Tell us the exact measurements of your current rollers, guides, or feed system, and we'll cut every length to match—down to the millimeter. No shims, no retrofits, no idle time while someone tries to force a square peg into a round hole.
Material blends are just as specific. Running abrasive stock that chews through standard rubber? We'll switch to a higher-durometer compound. Need more grip on coated paper without marking it? That calls for a softer surface with a textured finish. Each batch is mixed and cured for your operating temperature and speed, not for a generic datasheet.
What you get is a drop-in part that behaves like it was designed alongside your machine—because it was. Keep your line running at full tilt, and stop babysitting components that were never built for the job.
Batch-Level Testing That Mirrors Real Operating Conditions
Many test protocols impose artificial constraints that a real deployment would never see. Batch-level testing flips that by running entire lots through the same sequence of load, thermal, vibration, and power interruptions they will encounter in the field. This approach catches interaction failures that isolated unit tests miss—like a voltage dip that only corrupts data when dozens of devices pull current simultaneously.
The key is to keep batch composition varied rather than homogeneous. Mixing units with different firmware revisions, connector wear levels, or runtime histories forces the test to expose margin erosion that uniform samples hide. Operators often discover that a batch passing every individual check still produces a handful of soft failures once the group is subjected to realistic start-stop cycles and ambient drift.
Batch-level results also feed directly into lot acceptance. Instead of relying on statistical sampling tables, you can make release decisions based on how the whole group behaves under conditions copied from actual customer sites. That reduces the chance of shipping a lot that looks fine on paper but degrades quickly when installed alongside other equipment.
Export Support Without the Usual Logistics Headaches
When you send goods across borders, the last thing you need is a tangle of freight forwarders, customs brokers, and warehousing partners who never seem to talk to each other. Our export support starts with a single point of contact who actually knows your shipment's history, current location, and next step. You won't chase tracking numbers across three different portals or wait on hold to find out why a container is sitting at the port. We handle the paperwork, coordinate inland trucking, and flag potential delays before they become expensive problems.
That means no more surprise demurrage charges or last-minute scrambles for missing certificates. We pre-check documentation against destination country rules, book space on reliable carriers, and keep a buffer for the inevitable port congestion. If something does go sideways, you get a straight answer and a clear fix, not a chain of forwarded emails. The goal is simple. Your product leaves on time, clears without drama, and arrives without you having to become a logistics expert on the fly.
FAQ
PTFE gland packing holds up well across a wide temperature range and resists nearly all aggressive chemicals. Its low friction surface helps protect pump shafts and valve stems from excessive wear, which translates into longer service intervals and fewer unplanned shutdowns.
We source raw PTFE from vetted suppliers and run each production lot through dimensional checks, density tests, and compression recovery trials. Only material that meets our internal tolerance bands leaves the facility, so buyers receive the same reliable performance order after order.
Yes. We offer food-grade PTFE gland packing made from virgin PTFE that complies with relevant sanitary standards. It is often selected for pumps and mixers handling edible oils, syrups, and active pharmaceutical ingredients where contamination cannot be tolerated.
Typical configurations work well at shaft speeds up to 10 m/s and pressures up to 20 bar, though the exact limit depends on the braid structure and break-in procedure. For unusual conditions, we can suggest a densified or graphite-impregnated variant to extend the operating window.
We cut and supply packing from 3 mm up to 50 mm square, and we can adjust the braid density, lubricant content, or jacket material on request. This helps plants replace hard-to-find cross-sections without changing gland housing dimensions.
Cut rings to the shaft diameter, seat them individually with staggered joints, and tighten the gland gradually while the equipment runs. Allow a short break-in period with slight leakage, then nip up the gland only enough to control the drip. This prevents thermal expansion from scoring the shaft.
Beyond the product itself, we offer practical guidance on packing selection, installation, and troubleshooting. Our export team handles documentation and logistics carefully, and we keep buffer stock for repeat orders so lead times stay predictable.
Conclusion
Few sealing materials earn their keep the way braided PTFE yarn does when acids, solvents, and hot process fluids are involved. The yarn expands slightly under load to fill the stuffing box, blocking the microscopic channels that normally let aggressive media leak past a shaft or valve stem. Because it is braided rather than extruded, the packing keeps its density while staying flexible enough to follow slight misalignment or continuous stem movement. That same braid structure also lets operators adjust compression in the field without losing seal integrity. For pumps, valves, and mixers, cross-section choice matters as much as material: square sections suit slow rotary shafts, while smaller square or rectangular profiles often work better for reciprocating valve stems. We stock the most common sizes and can supply non-standard dimensions without forcing you to change the housing or gland follower.
Beyond standard stock, custom lengths and blended yarns are available so the packing matches the actual fluid, temperature, and shaft speed in your plant. Some blends add graphite or aramid for better heat transfer and wear resistance; others use food-grade PTFE where incidental contact is a concern. Each production batch is tested under conditions that mimic real operation—thermal cycling, pressure spikes, and dry start-up—so the packing is not just certified on paper but proven in the box. On the export side, we handle documentation, packing lists, and consolidated shipping without turning a simple order into a project. That means replacement packing reaches your maintenance team with the same lead time as a domestic purchase, while the material itself stays consistent from one batch to the next.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com