OEM Roll Forming Machine Supplier for Reliable Custom Profile Production
2026-10-17
When custom profiles demand precision and consistency, partnering with the right OEM roll forming machine supplier makes all the difference. Beenew has built a reputation for engineering reliable systems that handle complex geometries without compromising speed or durability. But what does it really take to turn a unique profile into a production-ready reality? Let’s explore the key factors that separate dependable suppliers from the rest.
Tailored Tooling That Matches Your Exact Profile Specs
Every profile has its own quirks—wall thickness, corner radii, material temper, even the direction of the extrusion grain. Generic tooling just can't account for those variables. Instead, we build each set of rolls, guides, and cutoff dies around the actual cross-section you're running, not a close approximation.
The process starts with your CAD file or a physical sample. From there, we map the profile's exact geometry and identify stress points where standard tooling typically causes marking or deflection. Then we adjust roll contours, entry angles, and support spacings to match those measurements—sometimes down to a few thousandths of an inch. The result is a tooling package that handles the profile the way it was designed to be handled, without forcing you to modify the drawing to fit the machine.
That level of fit means less time spent shimming and tweaking on the shop floor, and more parts coming off the line that look identical from the first run to the last. No flaring, no twist, no unexplained scratches. Just clean, repeatable profiles that match the spec exactly.
Production Uptime You Can Actually Count On
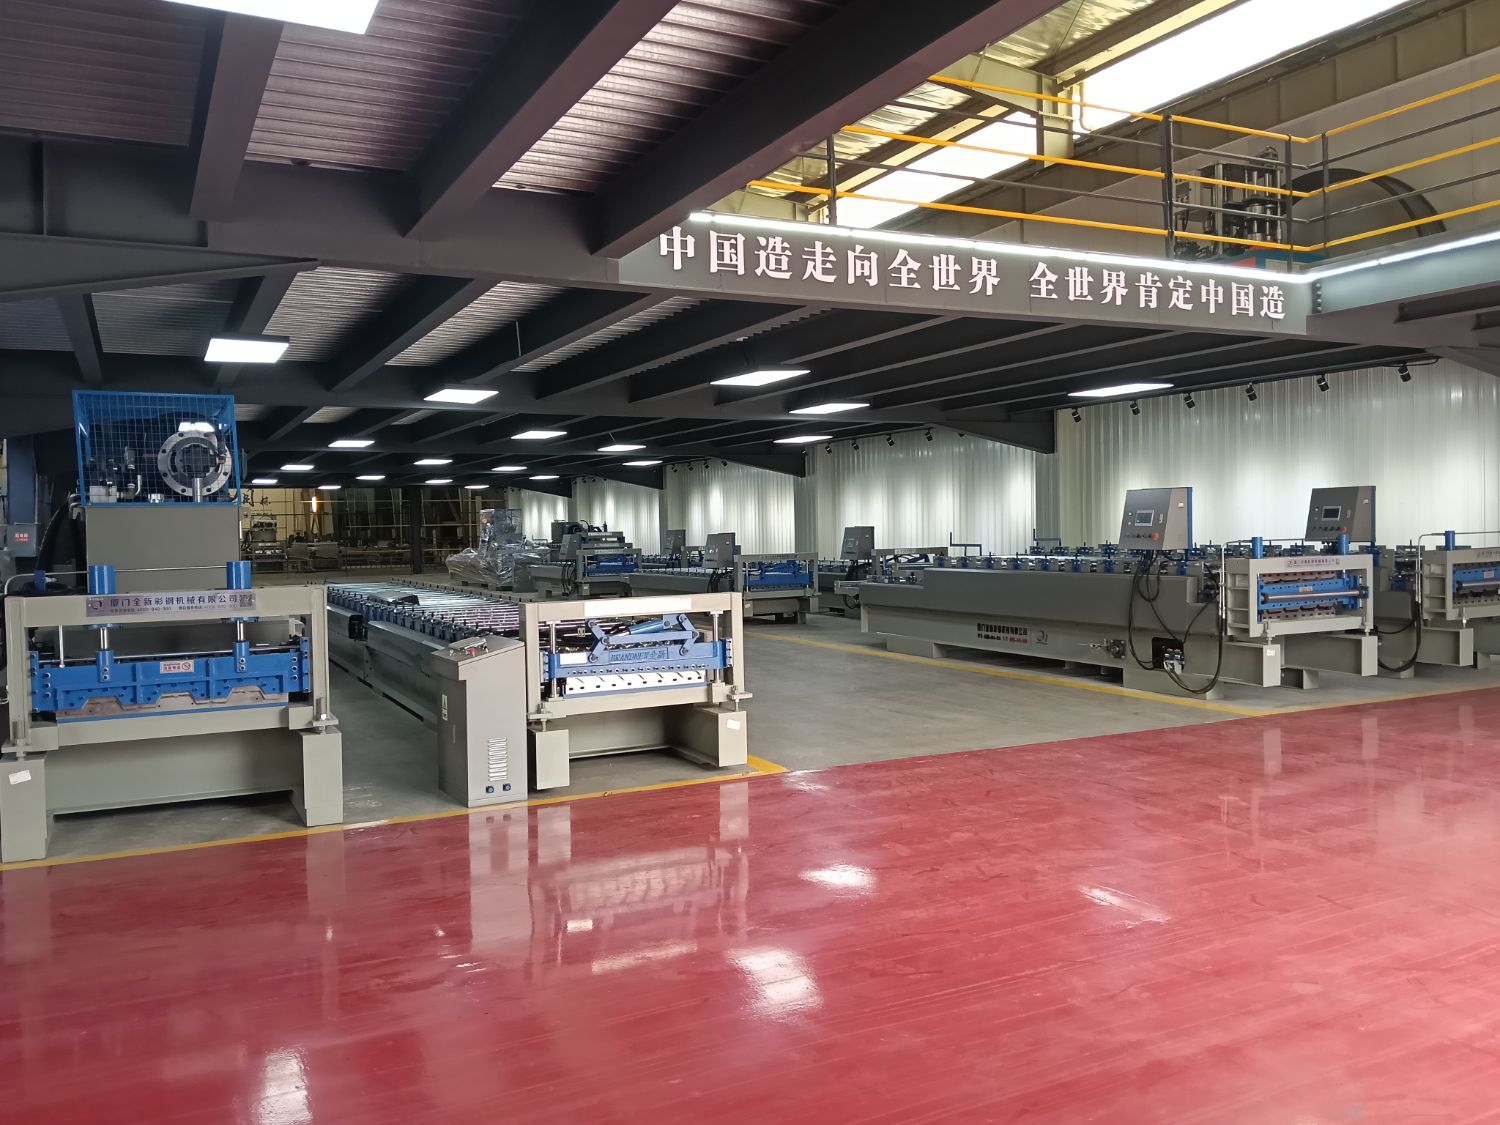
Most uptime guarantees fall apart the moment your facility stops matching the vendor's test environment. We build for the messy reality of production floors—variable power, aging infrastructure, operators who override settings to meet a deadline. Redundant control paths and automatic failover aren't add-ons here; they're wired into the base architecture, so a single failed sensor or a brownout doesn't cascade into a line stoppage.
The difference shows up in the details. Our systems watch for drift in motor current, hydraulic pressure, and thermal load, and they adjust parameters before thresholds are crossed. When a chiller started losing efficiency on a Friday afternoon, the system rerouted cooling demand and flagged the unit for a Monday morning service—no alarm, no lost production. That's what happens when uptime is engineered around how plants actually run, not how they look on paper.
What you get is a number you can plan around. Teams stop treating every shift as a potential fire drill and start trusting the schedule. If a supplier's uptime claim can't survive a power flicker or a rushed tool change, it's not uptime—it's marketing. Ours holds up under the conditions you already have.
From Coil to Cut-Off: One Seamless Workflow
The moment a coil hits the loading ramp, the entire sequence kicks into motion without a single pause. Decoiling, leveling, feeding, and measuring happen in one continuous pass, so the material never sits idle between stages. That constant motion changes how shops think about throughput—it’s no longer a series of handoffs but a single, self-adjusting run from raw coil to finished blanks.
What makes this flow truly seamless is the way the cut-off step reacts to the material in real time. Sensors read thickness and flatness on the fly, adjusting the shear cycle to match the exact coil condition instead of relying on preset timers. As a result, operators aren’t chasing small variances; the system absorbs them and still delivers clean, square cuts at the end of the line. The payoff shows up in less scrap, fewer rejected sheets, and a shift that ends without a pile of half-processed remnants waiting for attention.
Material Versatility Without Sacrificing Precision
Switching between aluminum, titanium, PEEK, and glass-filled nylon usually forces a trade-off: you either chase tight tolerances or accept whatever your machine can handle. Here, the process is built around the idea that a 0.005 mm tolerance shouldn't disappear just because the material changes. Toolpath strategies, feed rates, and thermal compensation are tuned per material, but the measurement routine stays identical across all of them. That consistency is what keeps a stainless steel bracket and a carbon-fiber housing on the same drawing—and inside the same tolerance band.
It's not enough to simply list dozens of supported materials. The real difference shows up in how the equipment behaves when you move from soft copper to hardened tool steel within the same shift. Rather than recalibrating between jobs, the system uses stored parameter sets that adjust for thermal expansion, chip evacuation, and surface finish requirements automatically. The result is that a prototype machined from acetal can be replaced with a production version in 17-4 PH stainless without redesigning the fixture or loosening the tolerance callouts.
Real-World Testing Before Your Line Ships
Shipping a product without exposing it to genuine usage conditions is like rehearsing a play in an empty theater. Real-world testing means pulling your line out of the controlled lab and into the messy, unpredictable hands of actual environments—dirt, humidity, rough handling, and the occasional user who ignores every instruction. It's not about simulating failure; it's about letting failure find you before your customers do. A jacket zipper that snags only when worn with a backpack, a mug that cracks in a dishwasher's top rack, a phone case that yellows under sunscreen—these discoveries rarely surface in standard QA checklists.
The value lies in timing. Run these tests while there's still room to adjust stitching, swap a coating, or reinforce a seam without derailing the production calendar. Send samples to a handful of trusted testers who match your target user's habits—not just colleagues, but people who will toss the tote into a car trunk, leave the water bottle in a hot car, or drag the luggage over cobblestones. Watch how the product ages in days, not years. The scratches, the stretched elastic, the fading print: each is data you can act on.
What separates meaningful real-world testing from a generic beta round is the questions you ask afterward. Don't just ask if they liked it. Ask what they stopped using after the first week. Ask what they almost returned. Ask what they would change if they had to live with it for a year. Then compare those answers against your own assumptions. The gap between what your team believes is durable and what actually survives a real commute, a real washing machine, or a real toddler is where your next iteration lives. Ship after you've heard that, not before.
Engineering Support That Extends Beyond Delivery
The moment a machine leaves our facility, our involvement doesn't end—it shifts into a different gear. We understand that real-world conditions are rarely as predictable as a lab bench, so our engineers stay on call to help you navigate the unexpected: a misbehaving sensor, a hydraulic quirk, or a software update that needs fine-tuning on your line. This isn't a scripted helpdesk; it's the same team that designed your equipment, now walking the floor with you until things run as they should.
What sets this apart is our habit of asking “what happens after the handshake?” Weeks or months later, we might reach out to check on throughput numbers or suggest a tweak that saves you a shift change of downtime. We’ve had clients call about a strange vibration and end up with a redesigned mounting bracket at no extra charge, simply because our engineer remembered how that particular frame flexes under load. That kind of continuity isn’t in a service contract—it’s in how we think.
Beyond repairs and patches, we treat every post-delivery conversation as a chance to learn. Your feedback on ergonomics, maintenance access, or tool wear feeds straight back into our next build. It’s not unusual for a customer to mention a small annoyance during a routine call, and then see that detail corrected in a later delivery before they even think to ask. That loop—from your floor back to our drawing board—is where the real engineering support lives.
FAQ
We start with your part print, material spec, and production target, then engineer the roll tooling, drive system, and cutoff around those inputs. The result is a line that forms your profile without forcing you to adapt your design to a stock machine.
Yes. We regularly build lines for asymmetrical shapes, deep draws, pre-punched holes, embosses, and multiple bends in a single pass. Send us a sample or CAD file, and our tooling engineers will tell you what’s feasible before any commitment.
We use servo-driven feeds, hardened tooling, and in-line straightening where the profile needs it. Every line goes through a dry-run and sample approval before shipping. That catches alignment issues early, so you’re not chasing scrap on your floor.
Cold-rolled steel, galvanized, stainless, aluminum, copper, and pre-painted coil are all within range, typically from 0.3 mm to 4 mm depending on yield strength. We match roll pass design to the material’s springback so the final angle holds.
Installation supervision, operator training, and remote diagnostics are standard. If you change a profile later, we can supply new roll sets and adjust the line rather than selling you a whole new machine.
Depending on complexity, plan on 10 to 16 weeks for design, tooling, build, and factory acceptance. Rush scheduling is possible for simpler profiles, but we don’t shortcut the sample approval step.
Yes, we often combine pre-punching, in-line notching, embossing, and hydraulic or servo cutoff in one pass. That removes secondary operations and keeps part-to-part consistency high.
A dimensioned drawing or CAD file, material type and thickness, annual volume, and any hole patterns or secondary features. If you only have a physical sample, we can reverse-engineer the profile and propose a tooling plan.
Conclusion
When you need custom profiles that fit your product exactly, working with an OEM roll forming machine supplier changes how smoothly everything comes together. Instead of adapting your design to a stock machine, the tooling is built around your profile specifications from the start, so every bend, flange, and radius lands where it should. That kind of precision carries into daily production too. The equipment is engineered for dependable uptime, not just impressive brochure numbers—real-world runs stay consistent without constant adjustment or surprise downtime that eats into your schedule.
Beyond the tooling itself, the whole line is designed as one connected process from coil feeding through final cut-off, which removes the usual bottlenecks between stages. Material changes are handled without sacrificing accuracy, whether you're switching gauge, coating, or tensile strength. Before anything ships, the line undergoes actual production testing with your profile, so you're not troubleshooting on your floor. And after installation, engineering support remains available—not just for emergencies, but for fine-tuning, training, and future profile additions. That full-circle approach is what makes a supplier a real production partner rather than just a machine source.
Contact Us
Contact Person: Sophie
Email: [email protected]
Tel/WhatsApp: 8615959271231
Website: https://www.beenew-rollformer.com/