Best Steel Mesh Welding Production Line for Efficient Manufacturing
2026-08-24
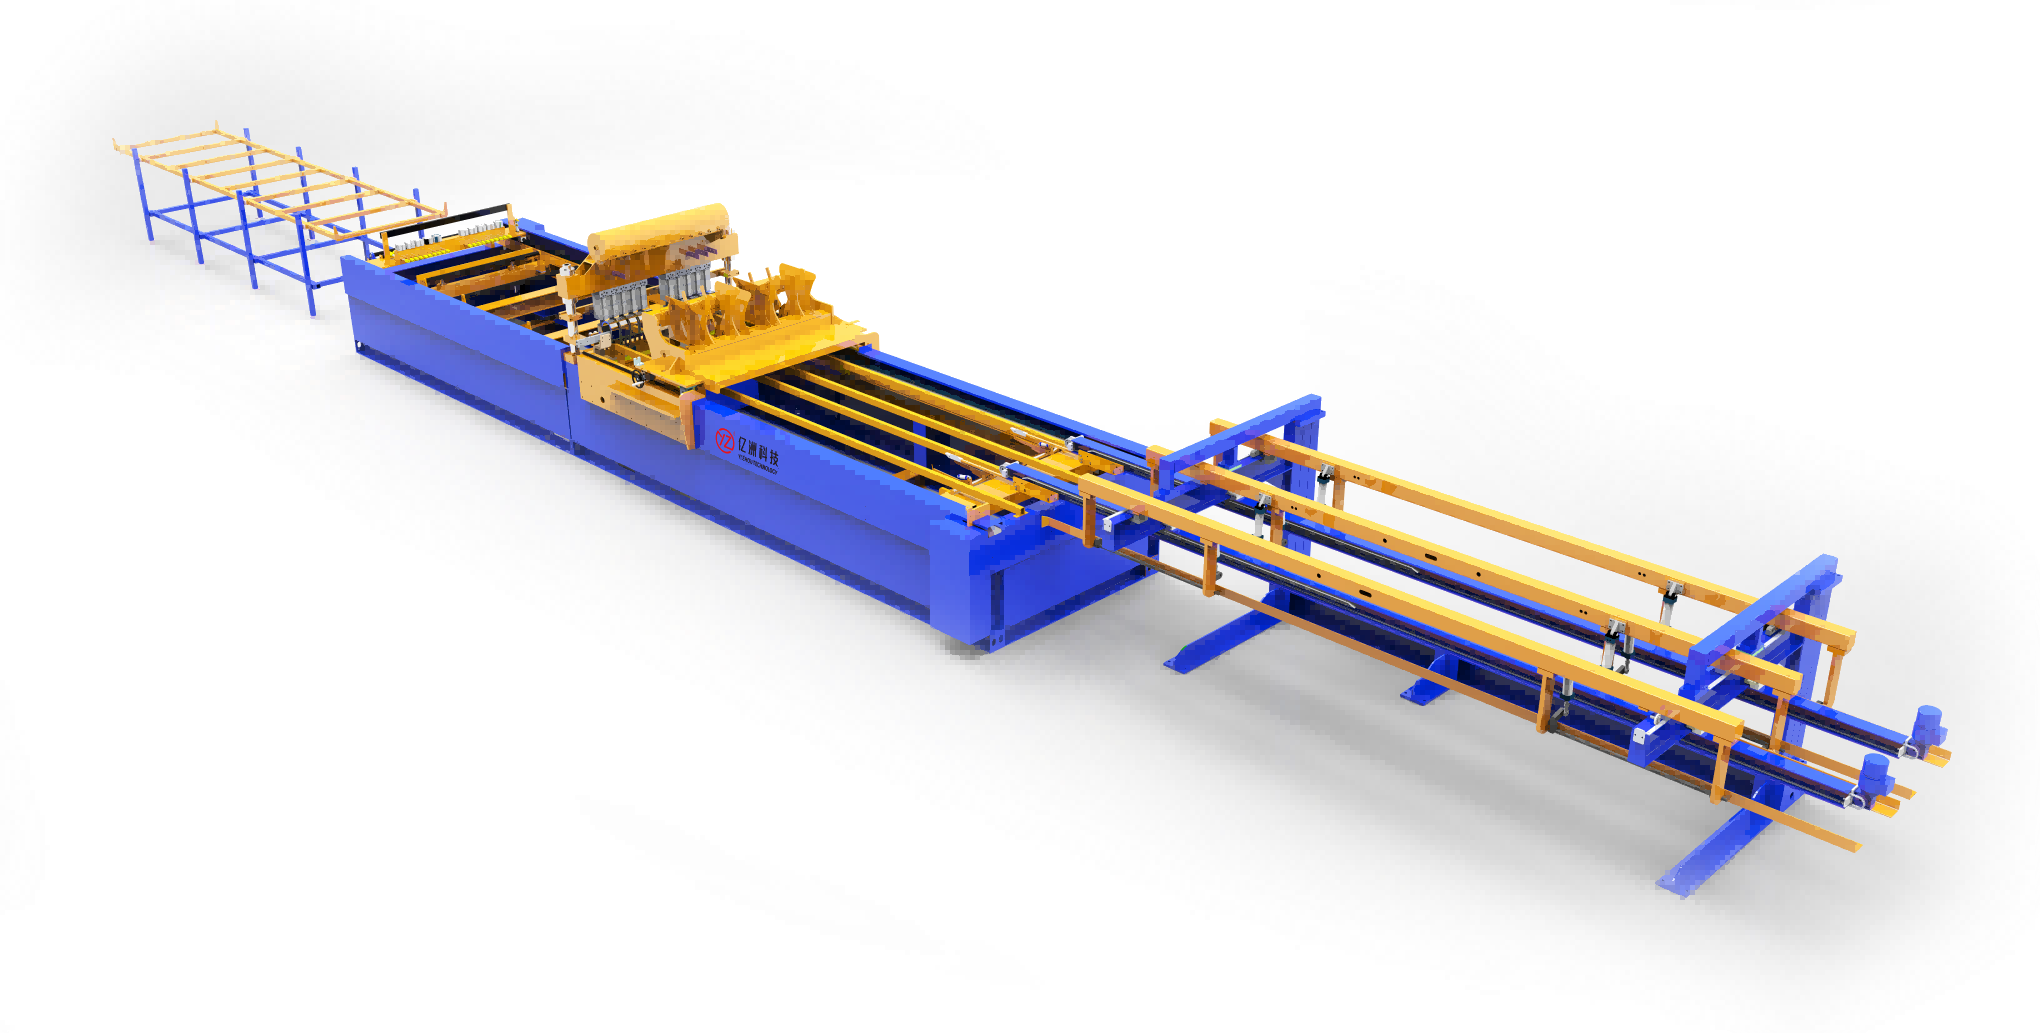
When every minute on the floor counts, the difference between hitting quotas and falling behind often comes down to one thing: your mesh welding line. The best steel mesh welding production line for efficient manufacturing isn’t just about faster cycles—it’s about repeatable precision, lower scrap, and uptime you can actually count on. That’s exactly where YI ZHOU TECHNOLOGY comes in. In this post, we’ll break down what separates a truly efficient setup from the rest, and why upgrading your line might be the smartest capacity decision you make this year.
Where Welding Precision Meets Material Savings
Getting a clean, consistent weld usually means burning through more filler metal and shielding gas than necessary. Our approach flips that logic. By fine-tuning arc characteristics and travel speed at the source, we hold dimensional accuracy within tighter bands while actually using less consumable per joint. The result reads on the inspection report and the material invoice at the same time.
The savings show up in ways you might not expect at first. Reduced spatter means less grinding and rework, so labor hours drop alongside raw material waste. Thinner heat-affected zones preserve the base metal's original properties, letting engineers specify lighter sections without sacrificing strength. Across a production run, those marginal gains compound into a measurable drop in cost per weld.
On the floor, operators notice the difference immediately. The arc stays stable through gaps and slight fit-up variations, so there is less need to compensate with extra wire or slower passes. It is precision that works with the realities of fabrication, not against them, and that is where the real savings live.
Faster Line Speeds Without Losing Weld Strength
Achieving faster line speeds in welding often comes down to controlling heat input rather than simply cranking up travel speed. When the weld pool gets too cold, penetration drops and the joint can look fine on the surface while hiding weak fusion underneath. Modern pulsed MIG and advanced waveform controls let you run hotter at the arc without overheating the base metal, so you can move faster and still keep the throat depth consistent.
Another piece that gets overlooked is wire feed stability. If the filler metal stutters or surges at high speed, you end up with uneven deposition and a weld that fails long before it should. Using a push-pull gun, properly tensioned drive rolls, and a high-quality liner keeps the wire moving smoothly, which means the arc stays steady even when the line jumps from 40 to 70 inches per minute. That stability is what preserves tensile strength when the pace picks up.
Finally, joint preparation and fit-up matter more at speed. A tight, consistent gap with clean edges lets you run a smaller, faster bead without resorting to excessive reinforcement to cover gaps. Shops that invest in better cutting and beveling often find they can increase throughput by 20-30% while destructive testing still shows the same break strength as their slower baseline welds.
Adaptive Controls for Fast Mesh Specification Changes
The real bottleneck in simulation workflows often isn't solving the model—it's reworking the mesh every time a geometry detail shifts. Adaptive controls change that by treating mesh density as a live parameter instead of a fixed setup. You can tighten the element size around a stress concentration, loosen it in far-field regions, and see the updated discretization in seconds rather than waiting through a full regeneration cycle.
Those same controls also preserve downstream setup when specification changes arrive mid-project. Boundary conditions, contact pairs, and material assignments stay mapped to the underlying topology, so a sudden switch from a coarse initial pass to a fine verification mesh doesn't force you to rebuild load cases. The mesher essentially tracks the intent behind the sizing, not just the current node distribution.
Teams handling iterative design loops benefit most here. A bracket gets thicker, a fillet radius grows, or a bolt hole moves—adaptive controls absorb the change and redistribute cells only where the local geometry demands it. That means fewer manual cleanups and fewer stale mesh artifacts that quietly skew results.
Lower Energy Use That Shows Up on the Invoice
A surprising share of a home's electric bill comes from things that aren't actually doing anything useful at the moment—chargers left plugged in, game consoles in rest mode, DVRs humming all night. Unplugging these or putting them on a smart power strip can lower the monthly kilowatt-hour total by 5 to 10 percent for a typical household, and that dip shows up on the very next invoice without anyone having to change their daily routine.
There's also a less obvious line item: peak demand. Some utilities charge extra based on the highest 15-minute draw each month, not just total consumption. Running the dryer, dishwasher, or EV charger during off-peak hours—or letting a smart thermostat shift cooling away from the early evening—can shrink that peak, and the bill drops even if overall usage stays similar. Over a year, shaving demand charges often saves more than replacing an old refrigerator.
Longer Maintenance Windows for Nonstop Production
Every manufacturer knows the frustration of shutting down a line for routine upkeep. Traditional schedules force you to squeeze inspections, lubrication, and part swaps into narrow gaps between shifts. By rethinking how maintenance slots are assigned, you can stretch those windows without sacrificing throughput. Instead of racing against the clock, teams gain enough time to inspect wear patterns, replace aging components, and run diagnostic checks that normally get skipped. The result is fewer surprise breakdowns and a steady rhythm that keeps orders moving.
Extending maintenance periods might sound counterintuitive when your goal is continuous output. The key lies in sequencing tasks so that no single asset stays idle for long. For example, staggered shutdowns let one section of the line rest while others keep humming. Technicians can then address hidden issues like belt tension drift or sensor calibration drift—problems that cause micro-stops when left unchecked. Over a quarter, this approach often yields higher overall equipment effectiveness than cramming everything into a two-hour Sunday window.
Another overlooked benefit is the reduction of rushed, error-prone work. When crews aren't pressured to finish before the next shift arrives, they take extra steps like torquing bolts to spec or cleaning cooling fins properly. These small acts compound into longer component life and fewer emergency call-outs. Pair longer windows with predictive data from vibration sensors or thermal cameras, and you'll catch failures weeks before they would have halted production entirely. The plant doesn't just keep running—it runs more predictably.
One System Handles Rebar Mesh and Security Fencing
Production lines often force a choice between structural reinforcement and perimeter protection, but this machine bridges that gap without missing a beat. The same feeding, straightening, and welding sequence that turns cold-drawn wire into load-bearing rebar mesh can be retooled in under an hour to punch out rigid security fencing panels. Operators swap the wire guides and switch the weld head pattern, then the machine runs either product at nearly identical speeds. That kind of flexibility keeps one piece of floor space earning its keep all year long.
What makes the dual capability work is the precision in the wire feed and the quick-change electrode spacing. Rebar mesh needs tight cross-wire contact for structural integrity, while security fencing demands clean, consistent openings that resist climbing and cutting. The system handles both by letting you set the longitudinal and transverse wire pitch from the control panel. No mechanical spreader bars to swap, no trial-and-error wire tensioning. The result is a panel that meets ASTM specifications for rebar and passes the twist-and-pry tests for high-security fencing.
Maintenance teams appreciate that the same spare parts box covers both product runs. The wire dereelers, straightening rollers, and weld transformer are shared, so there is no separate inventory for a second machine. When the schedule shifts from a highway bridge job to a utility substation fence order, the switchover is mostly a matter of loading the right wire diameter and calling up a saved recipe. That recipe system also stores your best settings for each material batch, cutting startup scrap to a few hundred kilos instead of a full shift of trial panels.
FAQ
The synchronized multi-electrode welding heads paired with a servo-driven mesh indexing system are the real difference. This combination cuts cycle time dramatically while keeping weld consistency across thousands of intersections per panel.
We rely on adaptive current control that reads the wire diameter in real time and adjusts pulse duration plus pressure automatically. No manual fine-tuning is needed when switching between gauges.
Yes, the fixture plates are quick-release and the controller stores up to 200 pattern recipes. A typical switch from a 50x50mm grid to a 100x100mm diamond pattern takes under 15 minutes.
Mostly electrode tip dressing and checking pneumatic seals. The self-lubricating linear rails and water-cooled transformers can run for weeks without attention. We suggest a 30-minute visual inspection per shift.
Absolutely, with a dual-gas shielding option. For galvanized wire, the system switches to a low-spatter waveform and increases pre-flow time to burn off zinc at the weld point, which prevents porosity.
The inverter-based power supply recovers braking energy from the mesh puller and feeds it back to the grid. Most plants see an 18-22% drop in kWh per square meter of finished mesh.
An integrated straightener with 12 rollers and a servo flying shear cuts wires to length with ±0.3mm tolerance. It feeds the cross-wire magazine automatically, so no separate cutting station is needed.
Light curtains, dual-hand start buttons, and a fully enclosed welding booth with fume extraction are standard. The PLC also monitors electrode force and stops the line if it deviates by more than 5% from the setpoint.
Conclusion
An efficient steel mesh welding line earns its keep in the details that don't make headlines. Electrode alignment, current ramp timing, and wire tension all have to work together, otherwise you bleed material through misaligned joints and weak spots. The best setups pair servo-driven weld heads with real-time current monitoring, letting the line run faster without trading away weld strength. When a shift switches from heavy rebar mesh to lighter security fencing, adaptive controls load the right parameters automatically, so changeover takes minutes instead of half a shift. Fewer rejects and less scrap wire mean the savings compound quickly.
Energy bills tell the story too. Inverter-based power supplies draw only what each weld needs rather than running flat out, and that shows up as a lower invoice month after month. Maintenance windows stretch longer with water-cooled transformers and quick-change electrode holders, which means fewer unplanned stops. And because one system handles both rebar mesh and security fencing without structural changes, you avoid buying separate lines for different products. That kind of flexibility—combined with lower waste, faster speeds, and predictable uptime—is what efficient manufacturing should look like.
Contact Us
Contact Person: Sophia Jiang
Email: [email protected]
Tel/WhatsApp: +86 17367381818
Website: https://yzwelding.com/